In This Article
What Makes a Minimum Viable Food Factory Operational?
A minimum viable food factory is the smallest complete operating cell that can receive materials, make the approved product, clean the system, release finished goods and dispatch orders. It is not the lowest-priced combination of production machines. Required utilities, product-contact interfaces, people, records and release responsibilities belong in the first phase, even when selected automation waits.
Start with one defined launch product and package envelope. Fund the functions needed to supply that envelope, then reserve specific expansion options. Remove speculative capability before removing a function on which saleable production depends.
An owner trying to reduce initial CAPEX may postpone the case packer or a second vessel. Those can be sensible choices. Postponing the only workable cleaning return, ingredient staging area or product-release responsibility is different: it leaves an incomplete operation. The design question is therefore where the first phase can be simpler while remaining coherent. This article follows a small liquid-food launch cell from vessel selection through its day-one handover, using a deliberately limited capacity illustration.
1. Define the Receiving-to-Release Cell, Not a Machine List
Write the initial commitment as a specific combination of products, packages, campaign quantities and delivery windows. A launch portfolio of one product family can require a different factory from a first phase intended to accept every future recipe. Product preservation and acceptance requirements must already have an appropriate technical basis; a smaller project does not lower that requirement.
Trace one commercial campaign through material receipt, preparation, processing, transfer, filling, packing, stock identification and release. For every handoff, name the incoming condition, the receiving function and who makes the relevant decision. This exposes functions that can disappear between equipment quotations. A tank supplier may assume prepared ingredients; the filler supplier may assume product arriving continuously in the required condition. Neither assumption creates the missing preparation or holding operation.
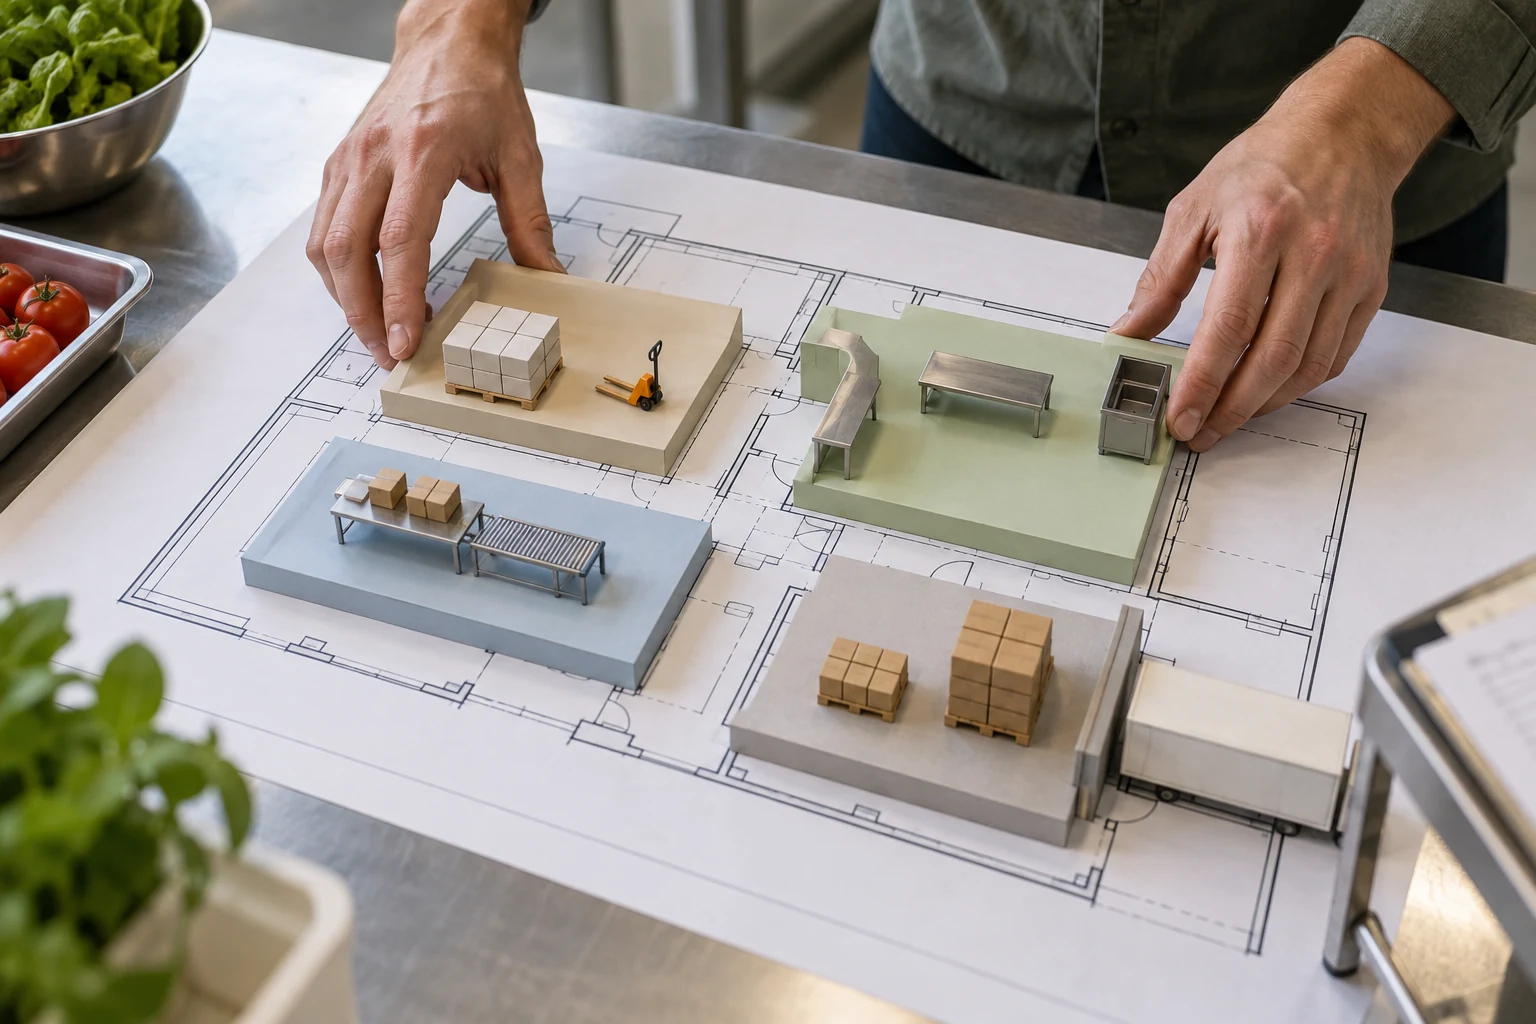
The result should be a compact operating-cell diagram with an assigned owner for each interface. Include the physical space where work occurs and the records needed to connect raw materials with finished stock. This is more useful for initial investment than a long speculative equipment schedule: it establishes which capabilities make the first sale possible. Functions outside that cell become later options unless the owner can explain why they are essential for launch.
For the example below, write the launch brief as: one approved liquid-food family, one 500 g pack, two 600 kg lots and 1,200 kg of finished product per day. Identify receipt, ingredient preparation, transfer/holding, filling and release for that duty. Any future product or package is a separately priced option.
2. Select a Vessel by Its Operating Role and Connected Systems
A vessel can prepare a batch, decouple two operations or hold released material. Those are different duties. State the useful working quantity, product behavior, required transfer condition and occupied cycle before choosing its nominal size. A larger shell does not automatically increase daily saleable output if filling or the approved calendar is limiting.
DPS’s tanks and vessels offering describes processing, fermentation and storage vessels coordinated with piping, CIP and controls. For a launch cell, that equipment discussion should therefore include the product inlet and outlet, cleaning supply and return, relevant instruments, isolation and the operating sequence. These interfaces are part of the vessel’s useful role, not optional detail to be discovered during installation.
Specify what the first phase genuinely needs and what is only a future possibility. For example, a reserved transfer connection may preserve a later option without buying an unused second vessel. Conversely, omitting the means to empty or clean the first vessel would not be a phase saving. Ask the equipment and engineering teams to show where their responsibilities meet, so the purchased package can become an operating system rather than an isolated asset.
Request a package arrangement showing overall height, product connection locations and the assigned cleaning connections. Add a supplied-by column for the transfer pump, connecting valves, instruments and control termination. A tank quote that leaves those items to others needs an owner and an allowance beside each interface before comparison.
3. Defer Automation Where the Manual Alternative Is Defined
The sensible comparison is a complete manual or simpler arrangement versus a complete automated arrangement. Manual secondary packing can be credible if staff, space, pack quality and material flow support the intended campaigns. A spreadsheet note saying “operator handles it” is not an operating design.
Describe the work cycle: what arrives, how often the task occurs, the physical handling, the check performed and where completed goods move. Test the busiest representative campaign rather than an average day. Include relief and the other duties assigned to the same people. The point is not to prescribe staffing ratios; it is to verify that the initial method has enough usable time and appropriate working conditions.
Preserve the future automated installation where it has a business purpose. Reserve a practical equipment route, the required space and an identified interface, with its initial cost shown separately. Avoid installing complete future capability merely because it appears in a mature-plant concept. DPS capital planning can compare these staged commitments against the launch baseline and later demand scenarios; the owner then chooses a defined tradeoff rather than a vague low-cost phase.
At the example's 300 kg/hour packing rate, 500 g packs imply 600 packs/hour. With twelve packs per case, the manual method must complete fifty cases/hour, or one every seventy-two seconds. Time case formation, loading, sealing, code checking and onward movement together before accepting that method.
| Function | Simpler Complete Launch | More Installed Capability | What Changes |
|---|---|---|---|
| Case packing | Defined manual packing and staging | Automated case-packing package | Labor cycle, machine feed and discharge interfaces |
| Batch preparation | One vessel with an achievable campaign sequence | Parallel preparation vessels | Cycle overlap, transfers and simultaneous utilities |
| Cleaning availability | Assigned cleaning window and complete circuit | Additional independent cleaning capability | Calendar, connections and concurrency |
| Operating confirmation | Defined operator actions and recorded decisions | More automated signals and sequence functions | Control ownership, evidence and exception handling |
4. Use the Whole-Cell Limit to Challenge a Larger-Vessel Purchase
Consider a hypothetical cell with a useful 600 kg batch quantity and a three-hour occupied processing cycle. Assume the stated calendar provides six hours for complete cycles, allowing two batches and 1,200 kg. The packing function is separately assumed to provide 300 kg per hour for four available hours, also 1,200 kg. Compatibility of the product, timing and intermediate handling is assumed for this teaching screen.
Replacing only the vessel allowance with a 900 kg batch quantity would create a calculated 1,800 kg processing capability over two cycles. It would not change the 1,200 kg packing limit. The complete-cell screen therefore remains 1,200 kg, and the extra process allowance is not automatically a useful day-one investment. The missing investment may be a downstream interface rather than a larger upstream shell.
Use the screen to direct the next investigation: can the approved campaign calendar or packing arrangement change, and is additional saleable demand available? Actual product trials, transfer behavior and operating requirements may change both calculations. The investment lesson is specific: before enlarging one machine, find the interface that stops the first-phase cell from creating more acceptable finished product.
A compatible eight-hour illustration might release lots at hour three and hour six, with packing at hours three to five and six to eight. That schedule requires an appropriate product handoff while the next lot is processed. Identify the holding/transfer function and its product constraints; the capacity minimum alone does not provide it. Review both handoffs before promising two released daily lots.
5. Build the Initial Utility and Cleaning Spine Completely
The launch cell needs utilities at the conditions required by its actual sequence. Map preparation, processing, cooling where applicable, packaging and cleaning against the same calendar. A connection sized from average consumption can miss a simultaneous event, while adding all nameplate loads can obscure which demands actually coincide.
Give each package a boundary schedule: supply condition, connection, return or discharge, controls interface and responsible party. For cleaning, a supply connection alone is not a complete circuit. The product-contact route, return path, relevant isolation and the means to observe the required procedure must be developed with the appropriate technical team. This article does not specify cleaning settings or establish a validated procedure.
In process engineering and design, DPS describes coordinated equipment documentation, layout, simultaneous utility analysis and controls specifications. For a minimum first phase, those deliverables can identify the smallest workable spine and the specific later connection points worth preserving. Keep the distinction sharp: a future branch may wait, but a function required to operate the launch circuit cannot remain unassigned. The scope should show both the complete first duty and the future option separately.
Issue the utility schedule by event, not only by equipment: ingredient preparation, product processing, filling and cleaning. For each event, list the required supply, its return or discharge and concurrent users. This lets the engineer examine the combined load instead of selecting infrastructure from an isolated package requirement.
6. Stage Site Readiness Before Promising First Production
DPS describes relocating Golden West Food Group's value-added food operation from Los Angeles to Fort Worth, coordinating receiving-site utilities, equipment movement, installation and startup validation while maintaining customer supply continuity in its published relocation account.
The dependency that matters to a first factory is the handoff into a prepared receiving site. Utilities and connection work must support the equipment arriving there; installation and relevant startup checks must support the first product sequence. A small launch cell has the same dependency, even when its procurement and construction circumstances differ from a relocation.
Turn that dependency into a release sequence. Before the vessel is called ready, its product outlet and cleaning return need assigned completed interfaces. Before the first lot is scheduled, preparation, packaging materials and the receiving filling function need to be available. Before finished stock becomes a customer shipment, the owner needs the agreed identification and release workflow. Each dependency can stop the operating cell despite completion of another package.
In the launch brief, put a responsible party and required evidence beside each handoff. This can change the initial investment: an additional buffer, field connection or operating resource may belong in phase one, while unused nominal vessel capacity may not. Prioritize the work that closes those handoffs before buying unused processing headroom.
7. Buy a Usable Handover with Explicit Interface Ownership
Make each package’s acceptance basis part of the procurement brief. Distinguish equipment checks, line-sequence checks, product evaluation and the owner’s commercial release. A successful pump or valve demonstration can establish a local function without proving that the complete product route is ready.
Prepare a short interface register for the launch cell, assigning the connecting work and evidence. The register should be specific enough to expose an omitted return, incompatible control signal or missing operator action. It should not become an indiscriminate checklist copied from a much larger plant. Focus on the boundaries through which the launch product and its supporting utilities actually pass.
Use this register during design reviews and handover. If a supplier changes a connection or the owner changes the package format, identify what must be reconsidered before accepting the campaign commitment. Keep the final drawings, relevant settings, operating instructions and agreed records available to the team that will run the cell. Those outputs allow the owner to operate what was purchased and understand what a later expansion changes, instead of depending on undocumented knowledge left with the installation team.
For example, if the first lot is ready but packing is unavailable, the handover must identify the permitted receiving state and the person authorized to change the sequence. Depending on the actual product basis, that may require a defined hold route or stopping the upstream operation, not an improvised storage decision.
| Boundary | Assigned Deliverable | Readiness Evidence |
|---|---|---|
| Vessel to filling | Transfer route and permitted sequence | Relevant line and product checks |
| Utilities to package | Defined supply/return connections | Confirmed operating conditions |
| Package to controls | Signals, actions and ownership | Sequence and exception tests |
| Finished stock to release | Identity and decision workflow | Agreed records and release responsibility |
8. Fund a Complete First Duty and Name the Expansion Trigger
The owner’s approval should distinguish three categories: complete launch functions, priced provisions for a credible later option and capability that is intentionally deferred. This makes the first investment reviewable without pretending the mature factory has already been funded.
Compare costs at the same boundary. If manual packing replaces automation, show the associated labor and stock flow; if a future vessel is postponed, show the initial duty the retained vessel must cover. Do not call an omitted necessary utility or an unowned release task a saving. The cost register should reflect an operating decision, not simply a smaller purchase list.
Define the evidence that would activate the next phase: sustained compatible demand, a demonstrated calendar constraint or a specific customer requirement. Connect that trigger with the time and work needed to add capability. The capital-planning engagement can then produce an initial equipment/utility scope, installed-cost basis and phased assumptions around the actual decision. The result should be a compact factory that can perform its first promised duty, with future commitments earned by evidence rather than purchased speculatively or concealed as unfinished work.
Make the deferred case packer a specific approval row: initial method at fifty cases/hour, completed task trial, assigned staff/staging, and the reserved later installation interface. If the next customer commitment exceeds the demonstrated manual duty, reassess the package and calendar before treating the deferred purchase as optional.
FAQ
Does minimum viable mean the fewest machines?
No. It means the smallest complete arrangement supporting the approved product and customer commitment. Necessary interfaces, utilities, cleaning, people and release responsibilities must still work together.
Can secondary packing remain manual initially?
Potentially, if the actual task, staff, staging and peak campaign are workable. Compare that complete method with automation rather than leave the activity undefined.
Does a larger vessel always increase output?
No. In the hypothetical example, packing remains at 1,200 kg/day even when one process allowance increases. The complete sequence determines useful output.
What should remain outside the first phase?
Capability serving only uncommitted future products or demand can be evaluated as a later option. Required launch transfers, utilities, cleaning and release functions cannot wait unless a complete approved alternative performs that duty.
What should be reserved for expansion?
Preserve specific justified options such as access, space or an identified interface. Price them separately from full future equipment and explain the demand trigger. Include installation access and the party making the later connection; a blank future area alone does not resolve either.
What should an initial engineering scope deliver?
A defined operating cell, equipment/interface register, coordinated utility and layout basis, acceptance responsibilities and an explicit boundary between initial work and later options.
Sources and Calculation Notes
Checked October 27, 2026. DPS case statements are attributed company reports, not independently audited performance. The numerical illustration is hypothetical; concept photographs are not project documentation.
- DPS — Tanks and Vessels — Offered vessel scope and connected piping/CIP/controls.
- DPS — Process Engineering and Design — Coordinated documentation, layout and utility analysis.
- DPS — Capital Planning and Feasibility — Initial scope and phased investment.
- DPS — Golden West Relocation — Attributed project-readiness lesson; no universal schedule or equipment inference.